1. Home
  2. Products
  3. H-Beams & Plate Girders
Automatic H-line · gantry SAWQ355B · S355JR · A572 Gr.50CNC drilled end plates

Welded H-Section Columns, Tapered Beams & Heavy Plate Girders

Submerged-arc welded H-columns and beams, tapered portal frame members, curved beams and plate girders. Webs to 3,000 mm deep, flanges to 1,000 mm wide, in Q355B, S355JR or A572 Gr.50.

3,000 mmMax. web depth
1,000 mmMax. flange width
6–100 mmPlate thickness
24 m / 60 tMax. single piece
01Engineering definition

The workhorse section, built to the exact size the design needs

A welded H-section is three plates: two flanges and a web. Hot-rolled H-beams stop at about 900 mm deep and come in fixed sizes. Welded sections can be any depth, flange width and thickness in our range, so the engineer sizes each member to its load instead of the nearest catalogue section.

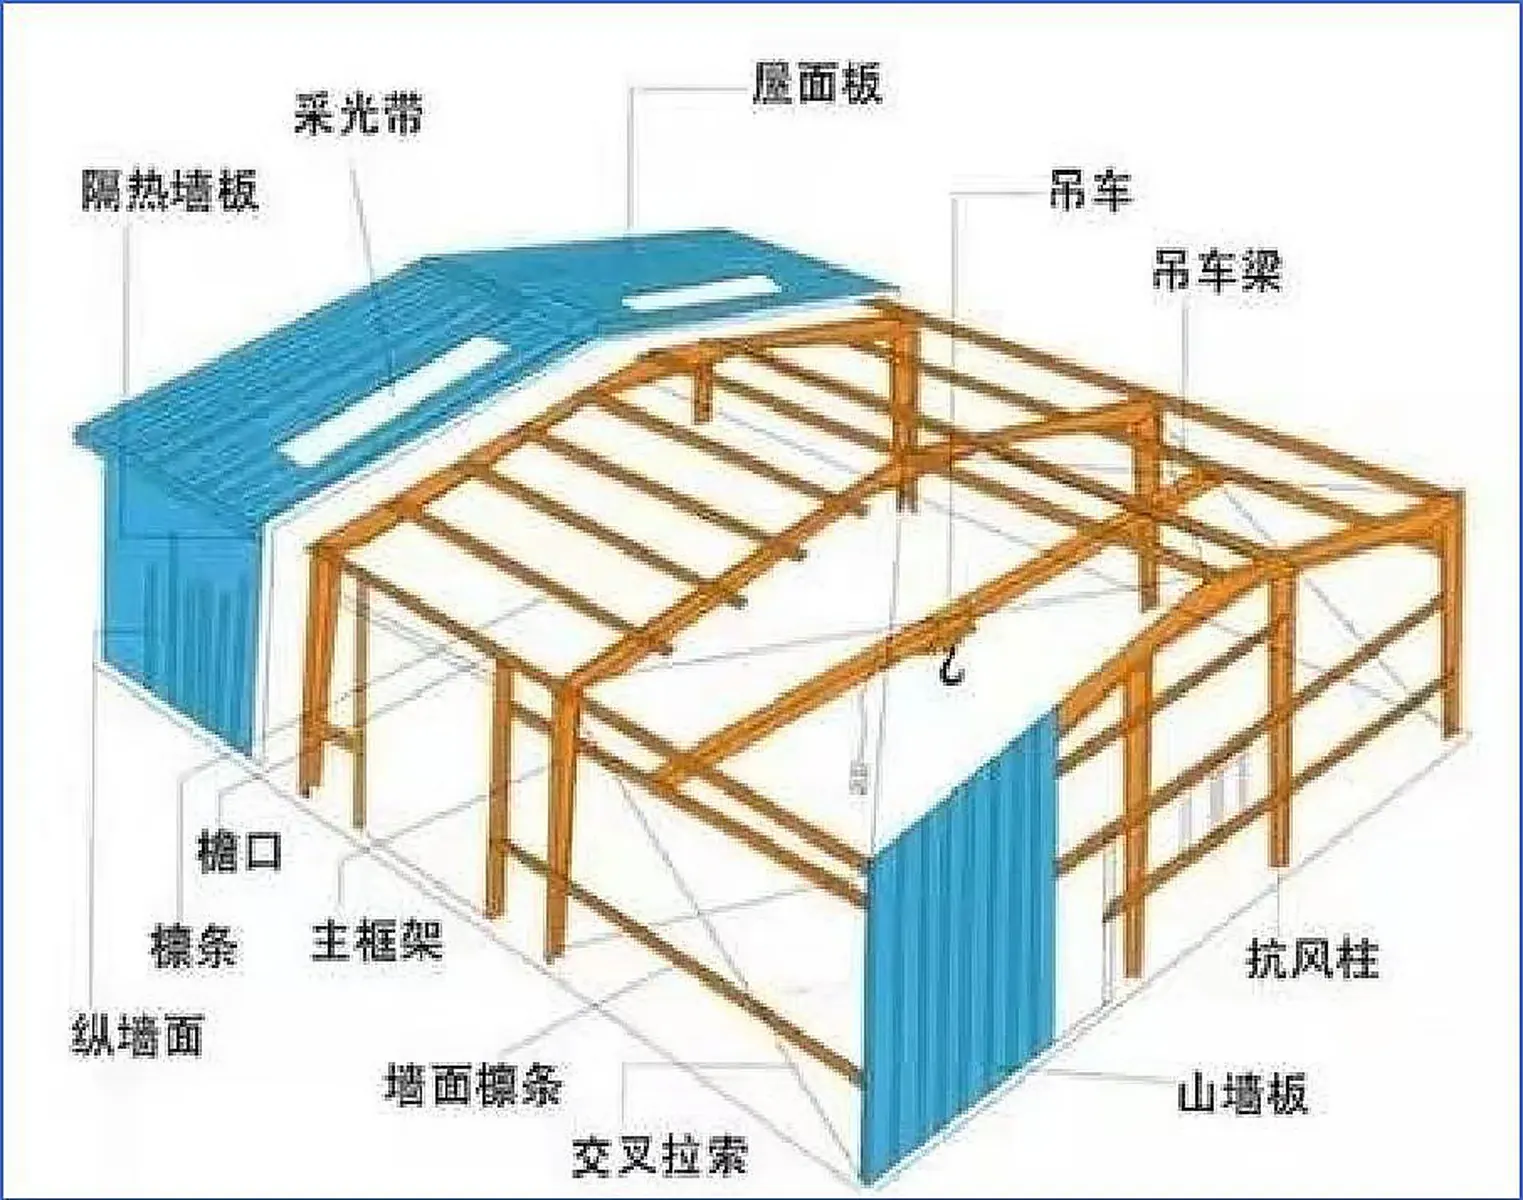
That freedom matters most in portal frames, crane buildings and transfer floors. Tapered rafters cut steel weight; deep plate girders carry loads that rolled sections cannot; thick flanges control deflection without going to a box.

Where rolled sections are the better buy, we procure them from mills and process them on the same lines: cutting, drilling, welding fittings and coating.

  • Welded H, tapered, curved and plate girders
  • Rolled sections processed where they are cheaper
  • Connections and end plates drilled by CNC
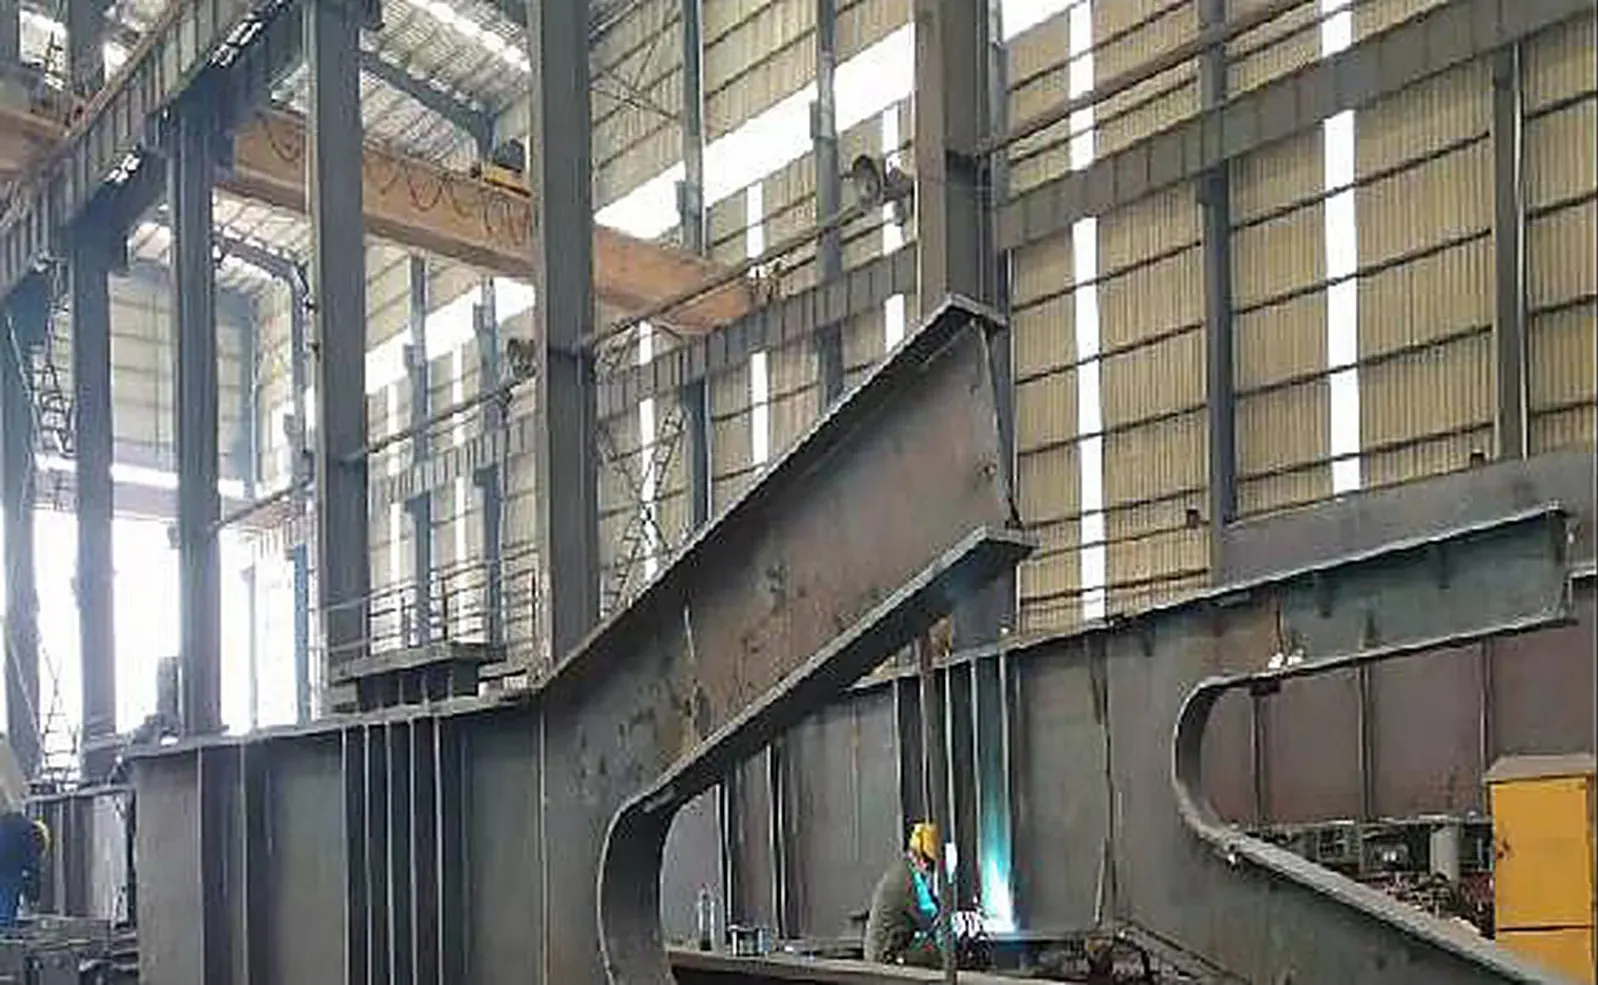
Welded plate girders after blasting
02Section types

Four H-section variants

Select a variant to see how it is made and where it is used.

Built-up H-columns and beams to 3,000 mm deep

Flange and web plates are strip-cut by CNC, assembled on an automatic H-line and welded with gantry SAW. Flange tilt and web camber are straightened on a flange-straightening machine before end cutting and drilling. Any section between rolled sizes can be made, so the design does not round up to the next catalogue size.

  • Web depth 200–3,000 mm, flange 150–1,000 mm
  • Plate 6–100 mm
  • Fillet or full-penetration web-flange welds

Variable-depth rafters and columns for portal frames

Tapered webs follow the bending moment, so warehouse and factory frames use 15–25% less steel than prismatic sections. Webs are nested on plate from the Tekla model to keep offcut low. End plates are cut and drilled in the same NC run.

  • Linear or haunched taper
  • Bolted end-plate connections, pre-drilled
  • Typical for 24–60 m clear spans

Arched roofs, canopies and curved façades

Curved beams are cut with a curved web profile and welded to bent flanges, or cold-bent on a section bender for smaller sizes. Each curve is checked against a full-size template on the assembly bed.

  • Radius checked against the 3D model
  • Segmented for transport with bolted or welded splices
  • Suitable for exposed architectural steel

Deep girders for bridges, transfers and crane runways

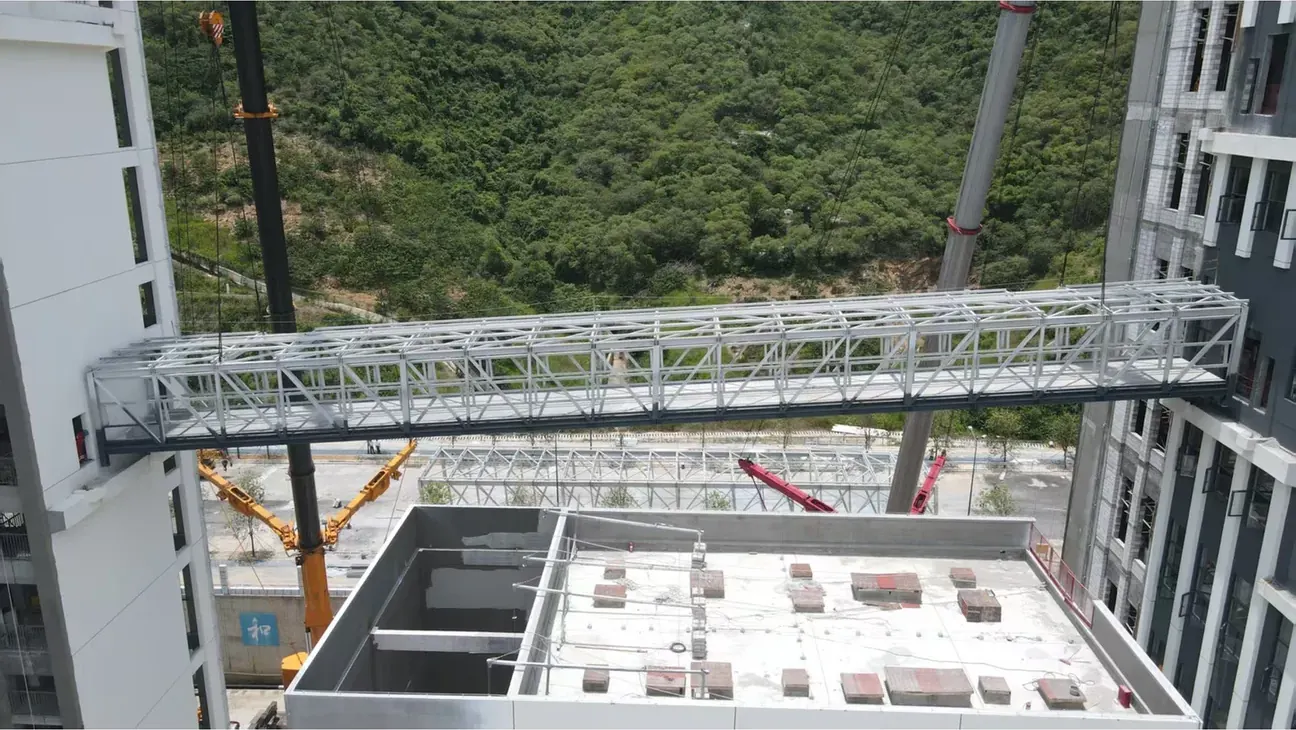
Plate girders use thick flanges and slender stiffened webs for spans and loads beyond rolled sections. Crane runway girders get full-penetration top flange welds for fatigue; bridge girders are pre-cambered and fitted with shear studs.

  • Bearing and intermediate stiffeners
  • Pre-camber to the design profile
  • Fatigue-rated details for crane girders
03Dimensional & processing limits

H-section and girder limits

Typical values for welded H-sections and plate girders. Tighter tolerances on request.

ItemLimitNote
Web depth200–3,000 mmAbove 3,000 mm as box or stiffened girder
Flange width150–1,000 mmUnequal flanges available
Plate thickness6–100 mmWeb from 6 mm; flanges up to 100 mm
Single piece length≤ 24 m11.8 m for 40HQ containers
Single piece weight≤ 60 tHeavier girders split at splices
Depth tolerance±2 mm (h ≤ 800) / ±3 mm (h > 800)Per GB 50205 / AWS D1.1
Flange tiltb/100, max 3 mmAfter straightening
Camber / sweepL/1,000, max 10 mmPre-camber to drawing where specified
Hole tolerance±1.0 mm group, ±0.5 mm pitch3D CNC drilling Φ12–60 mm

Tolerances per GB 50205, AWS D1.1 or EN 1090-2 as specified on the drawings.

Plant limits that apply

ItemCapability
Welded H-beamsWeb depth 200–3,000 mm; flange width 150–1,000 mm; plate 6–100 mm
Steel gradesQ235B–Q460, Q355GJ, Q420GJC; ASTM A36 / A572 Gr.50 / A992; EN S235–S355J2 / NH
Max. piece length≤ 24 m in the shop; ≤ 11.8 m for 40HQ containers; full length by break-bulk
CuttingCNC flame / plasma 6–150 mm; tube profile cutting Φ60–1,500 mm
Drilling3D CNC drilling Φ12–60 mm
Welding processesSAW, GMAW (CO₂), electroslag (ESW), robotic welding
Lead time25–40 days (standard members) / 40–60 days (complex members) after shop drawing approval

Typical values. Final limits are confirmed per project in our quotation.

Full plant limits for every member family are in the capability table.

04Materials & welding

Grades, toughness and SAW welding

The default grade for H-sections is Q355B, equivalent to S355JR and ASTM A572 Gr.50. Secondary beams and light frames use Q235B (S235JR / A36). Crane girders and members in cold climates are specified in Q355C or Q355D for impact toughness at 0 °C or -20 °C.

Web-to-flange welds are made by gantry SAW on both sides at once, which balances heat input and keeps the flange square. Where the engineer calls for full penetration, such as crane runway top flanges, webs are bevelled and back-gouged before the root pass.

JointProcessTest
Web-flange filletTwin-head gantry SAWVisual 100%, MT sample
Web-flange CJPSAW after back-gougingUT 100%
Flange and web splicesSAW / GMAW (CO₂)UT 100%
Stiffeners, end platesGMAW (CO₂)Visual, MT sample
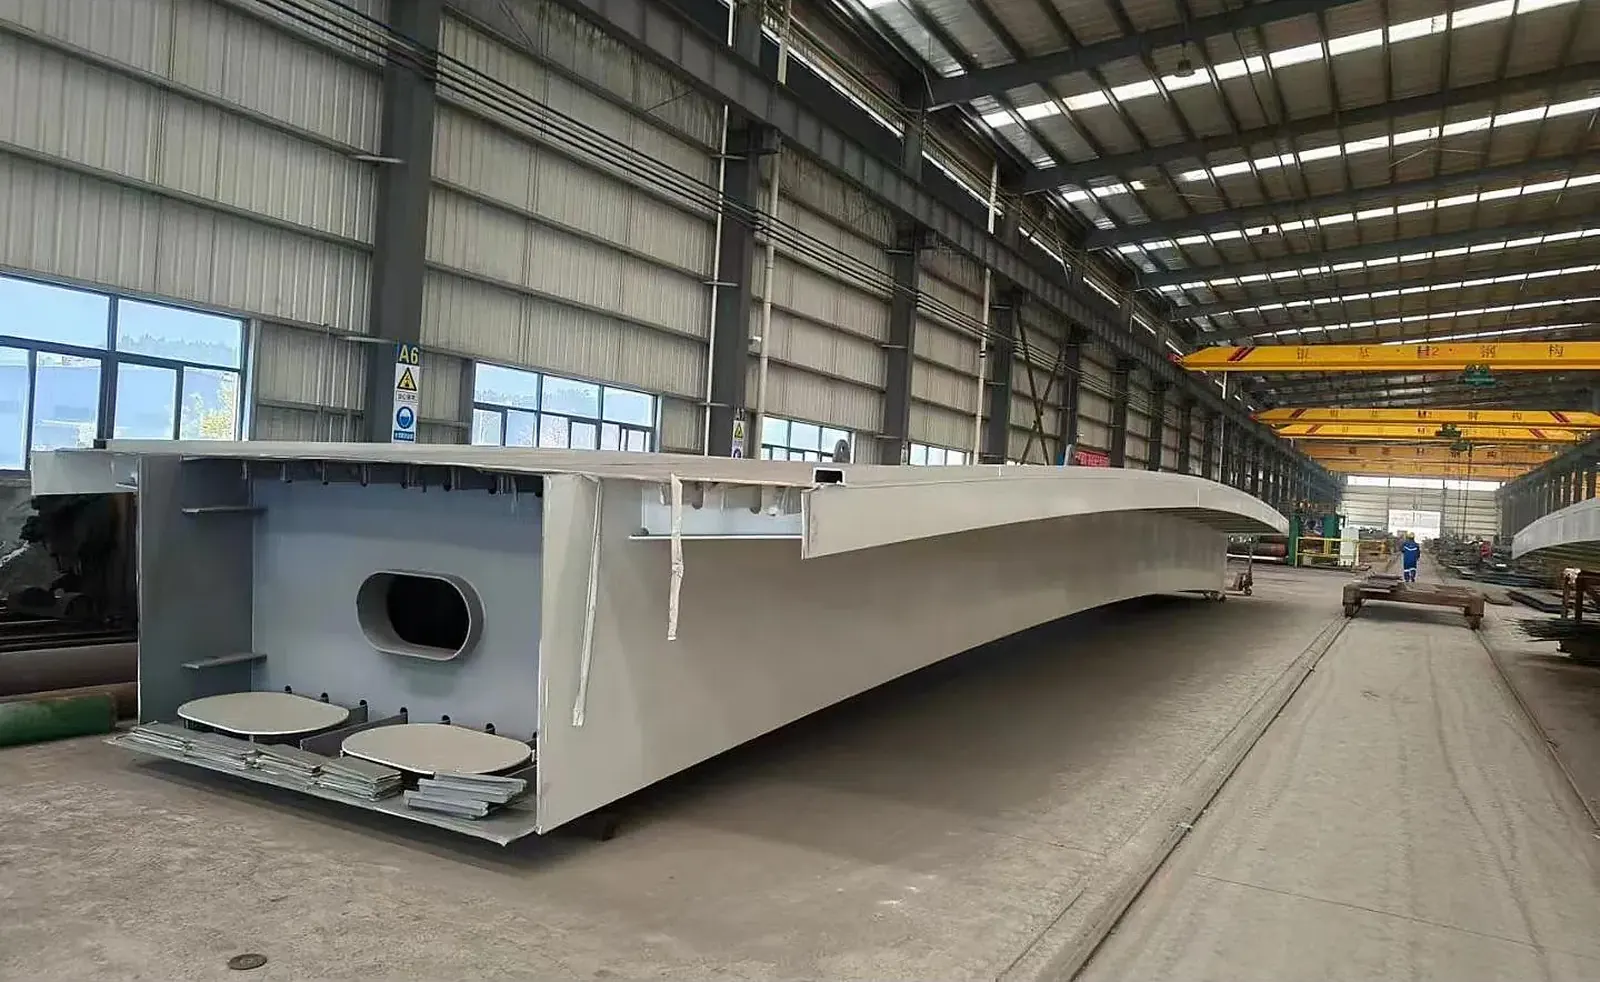
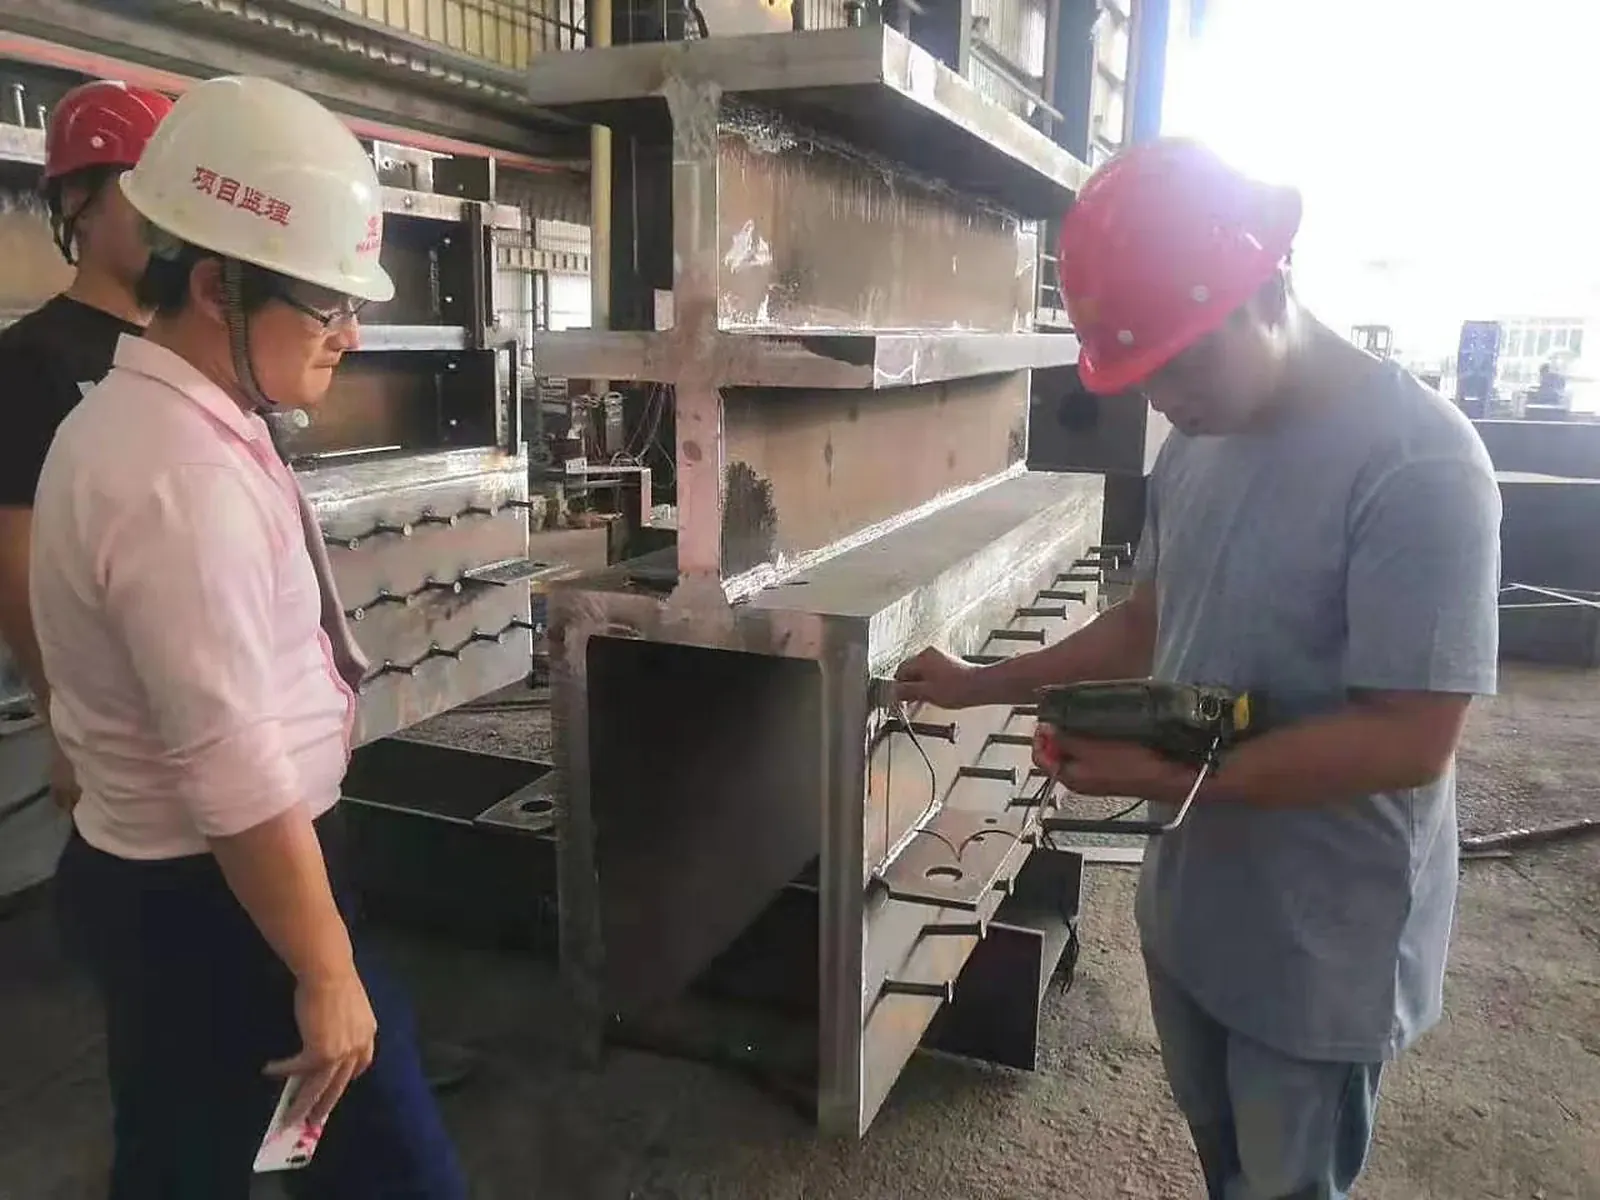
Welded H-sections at inspection
05Quality control

Checks on every H-member

Inspection records are filed per piece mark and issued with the shipping documents.

Section check

Depth, flange width, tilt and web flatness measured at both ends and mid-span.

100% UT on CJP welds

All full-penetration splices and crane girder flange welds tested and recorded.

Hole position audit

Bolt groups checked against NC data before the member leaves the drilling line.

Piece-mark records

Dimensional, weld and coating reports filed per piece mark, MTC 3.1 attached.

Related services

Tekla model, connection design, shop drawings, NC files and a weight-accurate BOM.

Sa2.5 blasting, epoxy zinc-rich systems, hot-dip galvanizing and intumescent coating.

100% UT on CJP welds, dimensional reports, MTC 3.1, packing and port logistics.

06Applications

Where this member family is used

Building systems where this member family does most of the work.

Tapered portal frames for 30–74 m clear-span logistics buildings.

Columns, rafters and crane runway girders for plants and workshops.

Plate girders for footbridges and link bridges.

Floor beams and transfer girders in composite frames.

Frames and trestle members for grain and bulk storage.

Build-to-print packages from 50 t for EPC contractors.

07Reference project

JD Asia No.1 Smart Warehouse, Dongguan

The JD Logistics Asia No.1 hub at Machong, Dongguan, uses a long-span welded H-section frame sized around automated sorting lines and high-bay racking. Frames were fabricated, coded and delivered in erection sequence to keep the logistics program on schedule.

The same tapered-frame approach was used for the Xiangxue Health Industrial Park (7,000 t, 30.6 m spans) and the Rrs logistics center in Foshan.

Related members

Box, tubular and tapered columns.

Pipe, box and H-section trusses to 90 m.

Multi-cell mega columns, Y/X nodes.

Patented permanent-formwork deck.

08FAQ

H-beam and girder questions

Send your drawings and our engineers reply within 24 hours.

Welded or hot-rolled H-beams: which should I order?

Hot-rolled is cheaper for standard sizes up to about 900 mm deep. Welded sections are better for deep, tapered or heavy members and when the design needs a non-catalogue size. We quote both where both work.

Web depth up to 3,000 mm with flanges up to 1,000 mm wide and 100 mm thick, single pieces up to 24 m and 60 t.

Typically 15–25% against prismatic sections for the same span. Single-storey warehouses usually land at 32–45 kg/m² of steel.

Yes, with full-penetration top flange welds, 100% UT, fatigue-rated stiffener details and rail clip holes drilled by CNC.

Q355B is the usual Chinese equivalent of A572 Gr.50 and S355JR. See our grade comparison chart.

Send your drawings. Get a 24-hour BOM and FOB price.

DWG, IFC, Tekla or PDF. Engineering review by our Tekla team, from 50 t or 2,000 m².